
6·
vor 3 TagenImage persistence also. I can get the IPS panel on my Thinkpad to display a ghost of an image on what’s supposed to be black space for upwards of a minute if I use the particular band of colors it seems to hate.
Progenitor of the Weird Knife Wednesday feature column. Is “column” the right word?
I make knives now, too. Why not buy one at flightlessforge.com?
Image persistence also. I can get the IPS panel on my Thinkpad to display a ghost of an image on what’s supposed to be black space for upwards of a minute if I use the particular band of colors it seems to hate.
You’ll say that right up until you have one right next to the other on the same desk. That’s what I have on my workstation at home, and my (admittedly, rather high end) OLED panel makes the IPS monitor look like cheap newsprint by comparison.
That, and even if you’re not considered part of whatever targeted group the current regime hates today, it doesn’t mean they won’t invent a new targeted group tomorrow that just so happens to include you.
This is before getting into all the false positive “identifications” of “criminal behavior” aimed at demonstrably innocent people e.g. as is already happening with the current Flock camera debacle.
No government has any legitimate reason to surveil its own citizens, and if any such excuse is generated to justify it in the beginning it is guaranteed to devolve into a tool of oppression afterwards. Once you give up rights there is no reality in which any government will voluntarily give them back.
Now I’m really curious. Did you make some sort of jig?
For adhesion, I prefer to apply a layer of Kapton/polyamide tape to my print bed. You can get it online in big square sheets — while using the typical 1" or 2" wide rolls one stripe at a time to cover the bed is technically possible, and I did it in the early days, it’s also a monumental pain in the ass and I advise against it if your budget can stretch to an additional two or three dollars to get the square stuff.
Forget glue stick. It’s messy, it produces an uneven thickness, the tubes dry out at inopportune moments, and it’s damn near impossible apply both evenly and also in an area that will actually correctly cover the entire footprint of your part. Instead, use cheap hair spray. Aqua Net seems to work best for me. The stuff in the pink cans; the absolute cheapest variety.
Note that on a Kapton surface your adhesion agent is also a release agent for certain materials, most especially Nylon and to a lesser extent PETG. Having that barrier in between your actual Kapton surface and your part will prevent it from molecularly bonding to your plate like the goddamned sword in the stone, forcing you to say several choice cuss words and re-tape your plate (as well as spend an entertaining afternoon scraping or sanding bits of Kapton tape off of the bottom of your print). Kapton and Nylon are both polyamides.
PLA, TPU, ABS/ASA, and polycarbonate can be printed directly onto bare Kapton depending on your level of audacity and/or bravery, especially in the case of the latter two. ABS is infamous for warping and the corners may lift off your bed without adhesive, or indeed even with adhesive… Even if the initial layer stuck to the plate perfectly well.
Note that you will have to raise your Z offset slightly if you apply tape to your bed. I.e., ideally by the thickness of the tape. You might find that you also want to raise your nozzle about 0.015-0.02mm if you’ve applied a layer of whatever adhesive, and lower it back down after you clean it off. Yes, the infinitesimally thin layer of hair spray will impact your first layer height provided your machine is accurate enough that its first layer offset is not a crapshoot on a per-print basis to begin with.
That sounds like a capital-N alignment Nightmare, so good on you for getting that figured out!
I think it’s less to do with retaining heat than the fact that the lower temperature printing materials like PLA and TPU will readily adhere even to a cold part, so the time in between nozzle passes is irrelevant. You could add to a PLA/TPU print with a layer time of 10 or 15 seconds or, if you prefer, tomorrow. In fact, with the zooty new printers when using PLA they have whole-enclosure forced air cooling to cool the part off as fast as possible to aid with overhangs and bridging, and prevent sagging when printing fast and thus at high(er) temperatures.
As you have observed, TPU has a ridiculously high layer adhesion in exchange for (or more likely, because of) its rotten temperature stability. It’s also very sticky as a result of its thermal properties, which is also why it strings so durn much.
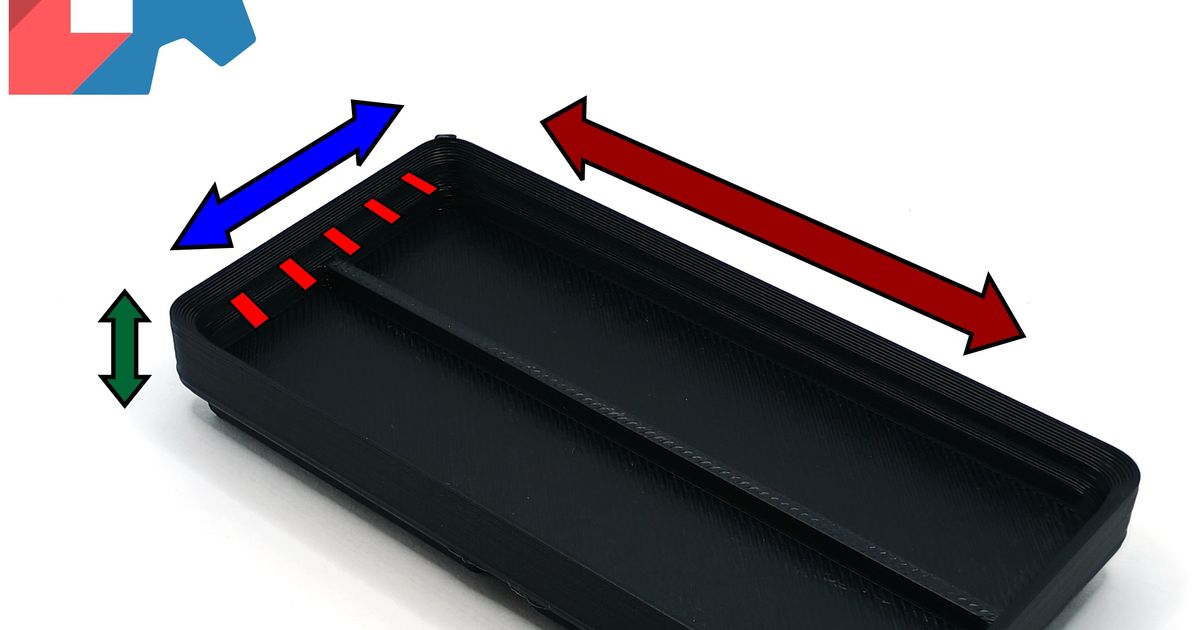
I dunno how OP did it but you can override your machine’s normal travel limit parameters in your slicer settings. Often the nozzle can physically travel further than the bounds of the build plate and is actually limited by hitting its rail endstops (or limit switches!) or striking some other part of your machine.
My Qidi can position the nozzle about 20mm beyond all four sides of the plate before it hits anything, but on the left and right sides it needs to be above z height 10mm or so to clear the Z axis gantries, and at the front and rear it’s just empty space. So you can’t print on the bed in that area because there is no bed. But if your object were shaped as such you could put overhangs out there in no man’s land. It would be risky, perhaps, but you could.

Ah, yes. Desperately falling back on making a tone argument of all things is a sure fire indicator that somebody doesn’t have a single leg left to stand on. Sony’s decades-long pattern of behavior does not put them in a position to be able to enjoy that luxury.
In other words: Get the fuck outta here with that.

I’ll save anyone else Googling it: A single new Boeing 737 costs around $100 million.
Meanwhile, when you order from Wish you will receive no order updates whatsoever. But they’ll send an email after three months asking you if by any chance your package happened to show up.
It’s fun, easy, and highly educational to build your own!
I freed up a couple of spare brain cells on that sort of thing back in the day once it was discovered around the schoolyard that Windows 95 (in addition to Office and a couple of other M$ products) would happily accept a CD key of all ones: 111-1111111. I don’t think this was applicable to the OEM versions, though. Windows 98 meanwhile would take a key of 12345-12345-12345, etc.
I still have the Windows 2000 MSDN CD key memorized. From XP onwards, the… alternative… activation methods did not require knowing license keys anymore.
One wonders what it was like to be a member of mankind in an era when all you had to memorize was actually useful information.
No, but I’ve done both polycarbonate and Nylon, or at least PA-6.
So far I’ve been getting the most use out of my Qidi X-Max 3, although it appears they’re no longer producing or supporting it. It predates the current multi-material schemes but it’s been able to print every funky high temperature engineering material I’ve tried to throw at it thus far. I’d really like to get some kind of tool changer machine to replace or supplement it at some point but it doesn’t seem like any of those are worth a damn for high temperature materials.

In the meantime I’ve just been using it to make stuff like this and driving myself bats with manual filament changes instead.
Well, it’s interesting to see that Seamonkey is still around. It’s what the Netscape suite mutated into before Firefox kind of became the main line descendant of that whole lineage. I used their WSIWYG web page editor back when I was a teen script kiddie and the state of the art in web design was still to use tables for everything.
I finally gave in and installed Waterfox on my own machine today. I hate to admit it, but having used it for my regular workflow (i.e. actually at work) for the last few hours so far it seems like what base Firefox should be. And arguably still was up until two or three years ago, although I suppose minus the Pocket integration BS that they were doing at that time.
The trouble with all of these forks is that they outright rely on regular Firefox to continue to exist upstream, and if Mozilla tanks and takes down Firefox as a whole all of the forks will by association go with it. I didn’t want to actually abandon Mozilla’s version because their user numbers seem to be tenuous enough as it is. But at this rate I think I’m going to switch our office over to Waterfox in the next couple of days regardless.
text entered
If this includes any information anyone enters into any type of medical service portal this is an instant HIPPA violation and these guys need to be federally prosecuted straight into the dirt. There may be other regulations that apply to this as well, e.g. those related to the banking sector. Never mind the inherent security implications in basically any workplace.
You do not log a user’s keystrokes or text entry. Ever. You know who does do that? Malware.
Yes, but I was fortunate enough to never actually get as far as ponying up the 99 cents. I got an MPX200 pretty early in my cell phone career which ran Windows CE and basically let the owner do whatever the fuck they wanted, including using .wav or .mp3 files as ringtones.
20 years ago was 2006. I will point out that at that juncture the original iPhone wasn’t even out yet. It released the following year. Normal people who were not turbo-nerds or high powered businessmen did not own smartphones in any significant number at that point.
If your device was even capable of downloading a cat video, we were still in the era when your cell phone carrier would have charged you $1.99 to do it.






We like Cellini.